
Evaluating the Condition of Pre-Owned Belting
Visual Inspection Criteria for Surface Wear
Most people judge a used belt by its worst groove. That is a mistake. Visual inspection of conveyor belting used in tough operations starts with surface wear, but not all wear is created equal. Look for cracking that runs deep, not just surface crazing. Gouges are bad. Glazing is worse.
Here is what catches my eye first:
– Uneven wear across the width, pointing to a misalignment issue.
– A shiny, hardened surface that has lost its grip.
– Exposed fabric or cords, which means the carcass is compromised.
If you see fabric, that belt has delivered its final verdict. The remaining lifespan is measured in shifts, not months.
Assessing Splice Integrity and Joint Strength
A splice reveals the true condition of any conveyor belting used in the field. A hammer tap along the joint exposes separation that the eye cannot see. Hollow sounds mean trouble. I look for skive marks showing a clean cut, and I check for excess rubber that hides a bad splice. If the splice steps are cracked at the base, that belt is done. Hot vulcanised splices outlast mechanical fasteners by years, but only when the joint was prepped right. I also flex the belt near the splice to expose hidden voids.
Some operators ignore this area. They focus on the cover instead. That is a costly mistake. The splice deserves closer attention. Here is what I check:
- Signs of moisture ingress around the splice edges.
- Warm spots that indicate friction build-up.
A weak joint turns good conveyor belting used in mining into a liability.
Measuring Remaining Thickness and Tension Capacity
When I evaluate pre-owned conveyor belting used in South African mines, I measure the cover thickness with a calibrated gauge, not a guess. The carcass holds the tension, and the cover protects it. If the cover has worn down to the fabric, the belt’s tension capacity drops fast.
I take readings across the full width, because wear rarely sits in one place. A belt that looks fine on the edges can be thin in the centre. The remaining thickness tells me how much life is left, but the tension capacity determines whether the belt can still carry the load. I compare the measured values against the manufacturer’s original spec.
Old conveyor belting used underground often hides its weaknesses. The numbers reveal the truth.
Identifying Heat or Chemical Damage
Heat and chemical damage do not announce themselves. I have seen conveyor belting used in Mpumalanga mines that looked intact until I pressed a thumb into the sidewall and it gave way. That softness points to oil exposure or solvent attack.
Heat creates a different damage pattern. Cracks appear along the flex points, often at the edge of the carcass. The rubber loses elasticity and takes on a glazed finish. I run a fingernail across the surface. If it flakes, the compound has degraded.
Chemical damage shows differently:
- Swelling or blistering that does not spring back
- Sticky surfaces that attract dust and grit
- Discolouration, from dark brown to a bleached white
Each clue matters when you assess pre-owned stock. The numbers from a gauge tell you thickness, but heat and chemical attack change the material itself.
Rekeying and Edge Damage: What to Accept
Rekeying ranks among the most misunderstood operations in material handling. Edge damage hides at the belt’s outer boundary, and I have examined conveyor belting used in Mpumalanga operations that looked beyond redemption at first glance. The deciding factor is the depth of the injury. Shallow scuffs along the rim accept a new key profile without compromising tension. Gouges that expose the reinforcement plies change the calculation entirely.
My acceptance criteria follow a clear order:
- Measure the distance from the outermost point of damage to the carcass line
- Check whether the edge retains a square, stable profile for the rekeying cut
- Confirm the rest of the belt shows no hidden softness or swell
When those conditions hold, rekeying restores a serviceable edge at a fraction of replacement cost. When they fail, the belt belongs in scrap.
Key Applications Across Industries
Aggregate and Mining Operations
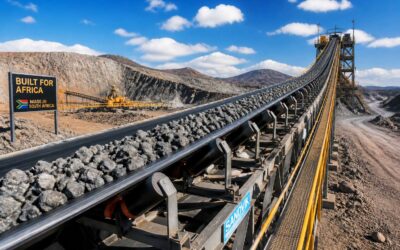
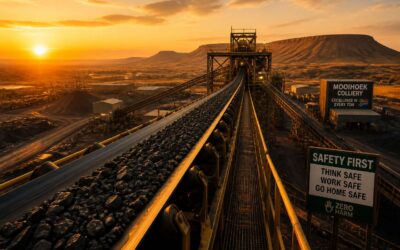
Mining adds roughly 7% to South Africa’s GDP, and almost every tonne of that material crosses a conveyor belt at some point. The conveyor belting used in aggregate and mining operations carries gold, coal, platinum, chrome, and the crushed stone that builds roads. These systems run for kilometres, often across terrain where truck haulage is impractical.
Consider the material streams at one open-pit operation:
- High-grade ore heading to the crusher
- Low-grade stockpile feed
- Waste rock bound for the dump
- Return fines from the washing plant
Each stream places a different strain on the system. The conveyor belting used in these conditions must cope with fluctuating loads, constant impact, and exposure to the elements. In quarries, the challenge shifts to wet aggregates and seasonal mud. Operators need belts that keep tracking despite the slop. A belt failure shuts down an entire plant, so reliability matters more than speed!
Recycling and Waste Sorting Lines
Recycling lines in South Africa face a brutal reality: the feedstock is chaos. Every bale, every bin, every bag carries metal shards, wet cardboard, and tangled film. The conveyor belting used in these sorting facilities must absorb punctures from bottle caps, abrasion from glass cullet, and the relentless torque of high-speed sorters.
I have watched a single misaligned belt halt a dual-stream plant outside Johannesburg. The cost in downtime exceeded the week’s profit margin. Different fractions demand different surfaces.
- Heavy ferrous scrap requires reinforced covers
- Light plastics need smooth, low-friction tracking
- Organic residues demand easy cleaning profiles
For operators, the conveyor belting used on waste lines is a compromise between grip and longevity. Unlike mining belts, these run indoors, but the contamination accelerates wear in ways that resemble chemical attack more than mechanical fatigue.
Agriculture and Bulk Material Handling
At harvest time in the Free State, conveyor belting used on grain elevators carries more weight per hour than any mining shaft. I have watched a mismatched belt shred itself on a sunflower seed elevator, losing bearing housings and costing a season’s profit.
The distinction lies in carcass flexibility and cover compound. Bulk crops require deep chevron cleats for steep inclines. Granular minerals demand smooth covers with impact resistance. For farmers and contractors, the right selection depends on a few measurable factors:
- Belt thickness
- Cover compound
- Cleat profile
These specifications determine whether your operation handles the surge or stops dead in the dusty afternoon!
Manufacturing and Assembly Conveyors
In a Gauteng assembly plant, conveyor belting used on a car door line must index with millimetric accuracy. The product variety across manufacturing demands precise control over friction and tracking. Unlike bulk handling, the concern is not tonnage but takt time.
For components moving through robotic workstations, the belting surface must tolerate sharp metal edges and hot weld flashes. These belts need a specific coefficient of friction to prevent slippage on inclined sections. I have seen the correct selection reduce production stoppages by an entire shift.
Consider the requirements:
– Uniform thickness for accurate indexing
– Static dissipative compounds for electronic assembly
– Reinforced edges against guide rail wear
The wrong choice leads to misaligned components and damaged tooling. Manufacturers select conveyor belting used in these processes based on material flow and product geometry. The belt becomes the heartbeat of the assembly line, dictating the rhythm of every workstation.
Cost-Benefit Analysis of Reconditioned Belting
Hidden Costs: Storage, Customization, and Downtime
Reconditioned belting often looks like a bargain until you factor in the less obvious costs. Storage alone can quietly eat into savings; reconditioned rolls need proper support and climate control, otherwise they deform before they ever reach a pulley. Customization is another expense. Standard widths and lengths rarely match your exact layout, so cutting and vulcanizing add labor and material waste. Then there is downtime. If reconditioned conveyor belting used in a production line fails prematurely, the resulting stoppage dwarfs the original price difference.
A careful assessment should include these variables, not just the purchase invoice. For example, consider these hidden cost triggers:
– Proper handling and storage equipment
– Splice kits and specialized tools
– Installation expertise and labour
– Extended lead times for custom widths
Each one shifts the balance between a genuine saving and a false economy. Ignoring them turns a prudent purchase into a costly experiment.
Performance Trade-Offs in High-Abrasion Settings
There is a moment in every procurement meeting when the reconditioned quote lands and the finance director smiles. That smile tends to die on the plant floor where high-abrasion settings eat optimism for breakfast. Conveyor belting used in these conditions carries hidden scars from its previous life, and those scars become your problem.
The cost benefit analysis only works if you measure replacement frequency, not initial price. A cheaper belt that fails in eight months instead of eighteen is not a saving, it is an invoice with extra steps.
Some operators run the numbers and reach clarity:
1. The upfront price looks tempting.
2. The wear rate erodes the margin.
3. The stoppage costs bury the original saving entirely.
Reconditioned belting has its place, but high-abrasion duty is a brutal judge of that decision.
When Refurbished Belting Is a Smart Financial Choice
Every procurement team has that one spreadsheet that tells the truth. Reconditioned belting wins when the application involves low abrasion, stable loads, and predictable duty cycles. The financial case collapses only when you confuse a bargain with a strategy.
Consider a logistics hub moving packaged goods. The conveyor belting used there faces none of the punishment found in primary crushers. Splices remain intact. Covers wear evenly. A reconditioned belt can deliver 80 percent of new performance at 50 percent of the cost. That arithmetic justifies itself. The conveyor belting used in such settings rarely tests the splice the way ore does. Inland freight depots and sorting facilities see steady, light loads that suit refurbished sections well.
The smart approach weighs three factors:
- Operational severity of the application
- Historical failure patterns from your own site records
- Cost per ton moved across the belt’s expected life
When the numbers favour refurbishment, they favour it loudly. The ledger always shows which side you are on.
Warranty and Return Policy Considerations
Warranty terms separate genuine reconditioners from opportunistic traders. The conveyor belting used in your operation deserves protection matching its intended service life. A refurbished belt with a robust warranty signals confidence in the process itself.
Return policies deserve equal scrutiny. Some suppliers offer partial credit based on remaining cover thickness. Others impose restocking fees that reduce the savings. Before purchase, confirm what documentation accompanies each roll. Certificates of reconditioning and test results support your position when disputes arise.
- Splice failure coverage is a common warranty exclusion
- Transport damage falls under some policies, not others
- Claim process timelines vary widely between suppliers
South African operations face unique logistics. In our experience, a warranty from a distant supplier costs more to enforce than one from a local reconditioner with technicians on standby. The conveyor belting used across your plant demands practical after-sales support, not promises in fine print.
Budgeting for Replacement Cycles
Few line items disappear faster than belting spend. Reconditioned stock changes the calculation, but only when you look beyond the purchase price. The conveyor belting used across a typical South African plant carries costs that hide inside each replacement cycle. Splice preparation time, production losses during changeover, and the salvage value of the old carcass all affect the final figure.
A cost benefit analysis should compare lifecycle cost, not sticker price. We price reconditioned rolls at 40% to 60% below new, yet the real saving emerges when you map the full service life. Budgeting for replacement cycles demands accuracy. A belt that fails early erases the discount.
- Track downtime cost per hour
- Factor in installation labour
- Compare cover thickness, not just rand per metre
Reconditioning stretches your capital. That simple truth makes the conveyor belting used in refurbished form a strategic choice for operations tracking every rand.
Where to Source Reliable Surplus Belting
Qualified Dealers and Certified Sellers
Sourcing reliable surplus belting requires more than a quick internet search. In South Africa, I always start by verifying a dealer’s track record. A qualified seller will openly share the belt’s origin, specifications, and inspection history. They won’t shy away from questions about storage or previous applications.
Certified sellers maintain proper facilities and follow manufacturer guidelines. When you evaluate sources, look for these indicators:
- Current industry accreditations
- Independent lab inspection reports
- Clear ownership documentation
These elements separate trustworthy vendors from opportunistic traders. The right dealer provides references from nearby mines or processing plants. Ultimately, sourcing conveyor belting used in your operation demands careful vetting. A small investment in verification pays off through years of trouble free service.
Online Marketplaces vs. Direct from Manufacturing Sites
Nearly a third of surplus conveyor belting advertised online in South Africa comes from unknown service environments. I have seen procurement teams buy rolls from marketplace listings without inspecting them, only to discover hidden splice damage weeks later.
Online marketplaces offer convenience and price transparency, yet the belt’s history is reduced to a stock photo and a short description. Direct from manufacturing sites, sellers can provide production dates, original specifications, and storage conditions. That traceability matters! When you need conveyor belting used in high-tension applications, the difference becomes obvious. A manufacturing source usually tests each roll before release, while online platforms rely on seller descriptions.
Questions to Ask Before Committing to a Purchase
Few buyers ask where a surplus roll has spent its working life, yet that answer determines whether the belt survives a single season or a decade. The most reliable sources keep maintenance logs and can name the exact conveyor belting used in each application. Start by requesting the original purchase order and any test certificates.
Before you commit, narrow your questions to what actually affects performance.
- What was the belt’s tension range and maximum load?
- How many splices exist and were they made on site?
- Has the roll been stored indoors or exposed to UV light?
Answers reveal far more than any photograph. A manufacturer’s surplus outlet typically provides these details without hesitation, while private sellers may deflect. Treat silence as a warning sign.
Sample Testing and Trial Runs
Sample testing and trial runs separate honest surplus from salvage. Conveyor belting used in a dusty Transvaal coal yard behaves differently from the same roll in a humid KwaZulu-Natal sugar mill. Ask for a cutting sample, 300mm square, and run your thumbnail across the cover. Cracks that open under light pressure indicate oxidative ageing, not abrasion.
Reliable sources allow trial runs under real load. I know one Mpumalanga contractor who rigs a short test loop with conveyor belting used in a local quarry before paying a cent. That practice reveals tracking issues and hidden internal damage that photos never show.
Consider these when evaluating a source:
- Does the seller allow on-site inspection?
- Can they supply a same-batch sample?
- Do they offer trial installation?
A seller with a physical yard in South Africa and a phone number that reaches a human will accommodate these requests. Private resellers with only digital photos and vague answers should make you walk away.
Shipping, Logistics, and Lead Time Factors
A reliable surplus belt starts with geography. In South Africa, the distance from a Johannesburg dealer to a Limpopo mine changes everything. Shipping costs can exceed the belt price itself. I once waited eleven weeks for a shipment from Durban that should have taken three. The port backlog ate my margin. Ask about lead times before you ask about price. A dealer who stocks locally can deliver in days. One who orders from overseas will keep you waiting months.
Verify the transport route. Cross-border permits and abnormal load restrictions add delays. Consider these factors:
- Check whether the seller holds stock in South Africa or ships on demand.
- Confirm the exact lead time in writing before you commit.
The best suppliers answer the logistics question without hesitation. They know that conveyor belting used in mining or agriculture is time sensitive. A stalled production line costs more than any saving on the belt itself.
Maintenance and Safety Considerations
Custom Fitting and Field Fabrication Techniques
One faulty field splice can idle a production line for half a shift! Field fabrication is where the durability of conveyor belting used in South African operations is proven. A vulcanised splice cured in a workshop behaves differently than one made in the open air of a Highveld afternoon. Safety protocols must account for this. Lockout procedures, pinch point awareness, and checking belt tension before knife work are not optional. They separate a routine repair from a lost finger.
Custom fitting demands precision with a tape measure. When cutting chevron profiles, the belt must be squared to within millimetres. Field fabrication techniques like step splicing require clean skiving and even pressure across the splice plate. Consider:
- Check ambient temperature before curing; cold rubber does not adhere.
- Align the belt centre line against the structure.
- Use a sharp knife, never a grinder, for the top cover skive.
I’ve learned the best conveyor belting used is only as good as the field splice. A poorly prepped surface leads to premature failure.
Installation Best Practices for Used Belting
Handling conveyor belting used on a previous line requires more than a visual check. The belt has already conformed to another structure’s geometry. During installation, allow it to relax and hang freely before making any cuts. A sudden release of stored tension can cause serious injury.
Safety starts with a clear lockout on every drive motor. Then verify the take-up carriage is in the correct travel position. Conveyor belting used in abrasive environments often has slight twists. Guide it over the idlers with a pry bar, never your hands. For the final connection, use a plate splice or vulcanised joint. Check the splice gap with a feeler gauge. It should be uniform across the width.
- Confirm all guarding is replaced before starting
- Run the belt under no load for one hour
- Monitor tracking every fifteen minutes
Routine Cleaning and Tracking Adjustments
Routine cleaning remains the first line of defence, because a dirty belt wanders. When debris packs under a return idler, it creates a high spot that pushes conveyor belting used in abrasive service sideways. Safety considerations are simple. Shut down, lockout, and then clean. Never reach for a moving idler.
Tracking adjustments follow a logical order. Do not guess.
- Measure the belt’s deviation from centre over five revolutions.
- Adjust the first idler group ahead of the drift.
- Let the belt run for ten minutes before tuning further.
Small changes produce the best result. Overcorrection creates a new problem, often a permanent curve in the belting. For conveyor belting used on an older structure, frequent checks early in the shift catch misalignment before it damages the splice.
0 Comments